Automation in Manufacturing: 7 Powerful Ways to Get It Right
Most discussions about automation in manufacturing begin with the wrong question. The immediate query is usually whether a manufacturer should automate a certain process, whereas the more important issue is the question of what processes should be automated, in what order and using which technologies.
This consideration is particularly relevant in the UAE, where local manufacturers are under growing pressure to embrace automation in manufacturing operations, due to the government’s drive toward economic diversification, the rising labor costs, and the scarcity of skilled workers who are willing to perform menial and dangerous tasks.
This note is aimed at decision-makers who are responsible for implementing automation solutions in their factories, bringing their production facilities to the next level. Industrial automation engineers, system integrators, procurement managers seeking to evaluate potential suppliers, original equipment manufacturers (OEMs) who provide turnkey automation solutions, and panel builders who install and commission control systems are the primary stakeholders for whom this information is beneficial.
It outlines the key characteristics of automation in manufacturing sector, describing its role, the technologies that can be utilized, and the implementation process, as well as the critical challenges that may arise.
What Automation in Manufacturing Actually Means
Manufacturing automation is basically using machines and computers to do production tasks with little help from people. This explanation is correct, but it does not tell the whole story. The thing is, manufacturing automation is not one thing.
A factory that uses a computer to control a conveyor belt and a factory that uses a big network of computers and robots to make things are both considered automated, but they are very different. It is helpful to think of manufacturing automation as having four parts, each one building on the one below it.
- Sensing and actuation is the part. This is the part. Sensors detect things like temperature and pressure and machines like motors and valves do something with that information.
- Control is the part. Special computers called logic controllers and programmable automation controllers make decisions based on what the sensors detect. They decide when to open a valve or start a motor.
- Supervision is the part where people can see what is going on and make changes if they need to. Special systems called SCADA and HMI let people see what the machines are doing and fix problems.
- Enterprise integration is the part. This is where the factorys computers talk to the offices computers so people can make decisions about production and inventory.
A lot of people get confused about how automated a factory is because they mix up these different parts. A factory can have good control, with fast and reliable computers running all the machines, but still have to enter production numbers into a spreadsheet by hand at the end of the day.
Manufacturing automation is what it is. It is good to understand what it can and cannot do. To plan for manufacturing automation, you need to figure out which part of it is the weakest, and that will tell you more than any salesperson will.
Manufacturing automation is what you need to look at. You need to look at the different parts of manufacturing automation to really understand it.
Placing Your Plant on the Automation Spectrum
Before comparing different solutions and narrowing the search scope to a group of potential suppliers, it may be helpful to assess where exactly the operation falls on the automation spectrum. The reason why it is important to do so lies in the fact that the most beneficial move forward is different for plants at various levels.
A plant at the manual level is characterized by having operators make most control decisions, and have no or very limited computer-automated control loops, with no data captured digitally beyond basic recordkeeping. A plant at the basic control level has programmable logic controllers for individual machines or production lines, but little to no connectivity between them, with each essentially operating on its own.
A plant at the level of supervised control has some form of SCADA or HMI that provides an overarching view of the production process. It is still controlled manually, but now there is one point of reference that allows for making adjustments in real time.
A plant at the level of integrated control has its supervisory level connected to enterprise resource planning and manufacturing execution systems, providing managerial and planning software with production data in real time automatically, without the need for manual entry.
Finally, a plant at the level of adaptive control, which is rare in practice, employs the additional layer of analytics that allows it to react to the data, by, for example, automatically stopping production when quality issues arise or predicting when maintenance will be necessary.
Most manufacturers in the region are somewhere between the basic control and supervised control levels, with some areas of the production process already utilizing integrated control, typically for individual machines or production lines that use predictive analytics.
This state is normal and should be used as a guide for what the automation in manufacturing should entail for the specific project, rather than attempting to design the fully adaptive control system from the outset.
Levels of Automation: Fixed, Programmable, and Flexible
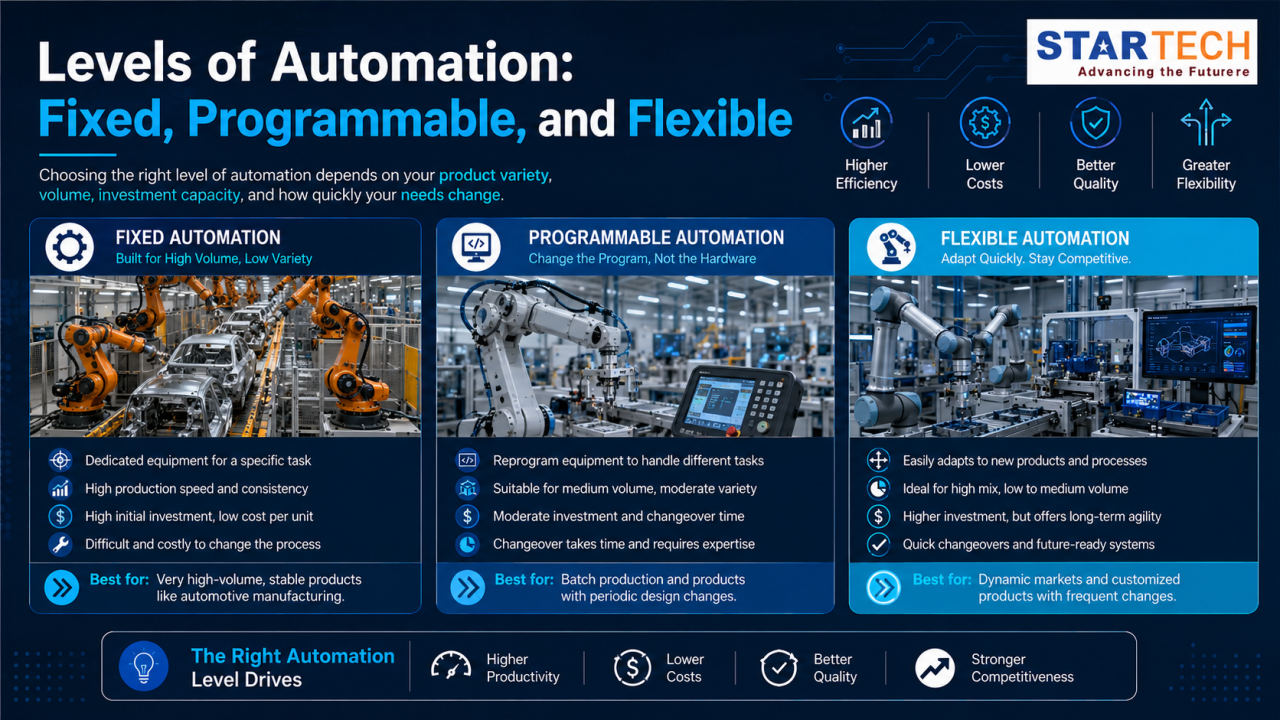
Not every production line needs the same kind of automation, and the differences go beyond budget.
Fixed automation is built for a single task and nothing else — a dedicated bottling line or a purpose-built stamping press, for example. It runs fast and cheap per unit once commissioned, but changing the product typically means rebuilding the hardware. This still makes sense for high-volume, low-variety production, which is common in packaging and basic assembly operations.
Programmable automation uses the same physical equipment to run different products by loading different programs — a CNC machine cutting different part geometries is a good example. Changeover takes longer than with fixed automation, but it is far cheaper than rebuilding hardware, which makes it well suited to batch production where product runs change every few weeks or months.
Flexible automation (sometimes called soft automation) goes a step further, allowing rapid changeover between products with minimal manual reconfiguration — often through robotics with interchangeable end-effectors, vision-guided systems, and software-defined processes. It costs more upfront but suits manufacturers dealing with frequent product variation, shorter runs, or unpredictable demand.
Choosing between these levels is a question of production volume, product variety, and how often the line needs to change — not simply which option is most advanced.
The Core Technologies Behind Manufacturing Automation
Programmable Logic Controllers and PACs are really important for machines to run safely and smoothly. These Programmable Logic Controllers handle tasks while PACs are more powerful and can handle tasks that need more control and connection to other systems. Programmable Logic Controllers and PACs are essential for the control layer executing the logic that keeps machines running safely and consistently.
SCADA and HMI systems are also crucial. The SCADA software collects data from Programmable Logic Controllers across a site giving supervisors and engineers a clear view of what is happening with production, alarms and trends. The HMI systems are closer to the machines giving operators the controls they need to run the equipment.
Industrial robots and collaborative robots are used for tasks. Traditional industrial robots are good for tasks that require a lot of speed and power like welding or moving things. They usually work inside an area. Collaborative robots, on the other hand, are designed to work with people without the need for a safe area. They use technology to limit the force they apply and have safety monitors.
Machine vision systems use cameras and software to check parts for defects, make sure things are put together correctly, read codes and help robots pick and place things. This technology is becoming more popular because it can be added to existing production lines without having to change everything.
Automated guided vehicles and autonomous mobile robots move things around a facility without a driver. Automated guided vehicles follow a path while autonomous mobile robots can navigate on their own using sensors and maps. This makes them more flexible, but more expensive.
Industrial sensors and the Industrial Internet of Things are also important. These sensors can track things like equipment condition, energy use and production in time rather than just checking occasionally. This data helps with maintenance and planning.
Manufacturing Execution Systems software tracks what is happening on the plant floor including work orders, quality records and production performance. It helps connect the plant floor to the rest of the business so investments, in automation can actually improve decision making. Manufacturing Execution Systems are often the missing piece that makes automation investments pay off.
Why Manufacturers Invest in Automation
Any serious consideration of manufacturing automation process must evaluate the trade-offs involved, since ignoring them is a sure way to engineer a disaster.
Upfront costs. Automated processes require a large investment in robotic machinery and control systems. However, the equipment cost is only one part of the equation – often a small one at that – since installing them and retrofitting existing infrastructure to work with the new systems takes much longer and is far more expensive than anyone expects.
Integration time and complexity. New automated systems rarely exist in a vacuum. Installing robots means integrating them with legacy machines and control systems, which is much harder than most realize. The skills required for maintenance and programming are specialized, so unless a manufacturer is entirely self-sufficient with its maintenance and repair work, it will have to hire contractors for any automated machinery-related job.
Fixed automation is less flexible but usually faster, requiring less time and effort to produce a single unit. However, it is much harder to repurpose if the manufacturer wants to shift to another product that uses a different production process.
The threat of cyberattacks via control system networks. Connecting automated machines into a network, whether it is a factory LAN or the Internet for remote access and control, creates possibilities for exploitation that did not exist when the machines were standalone. Industrial control systems were never designed with security in mind, and that constitutes a risk to any manufacturer that connects them to a network, whether they realize it or not.
Downtime during installation or upgrades. Upgrading to a new automated process is seldom something a manufacturer can do without any production downtime, and that downtime always turns out to be more costly than budgeted. It can easily outweigh the benefits of automation during the first year or two after installation.
With all of these issues in mind, it should be apparent that automation is not a risk but rather an opportunity to be seized. The next section will discuss how the risk of those potential pitfalls can be reduced by preparing a realistic automation budget.
The Real Costs and Limitations of Automation
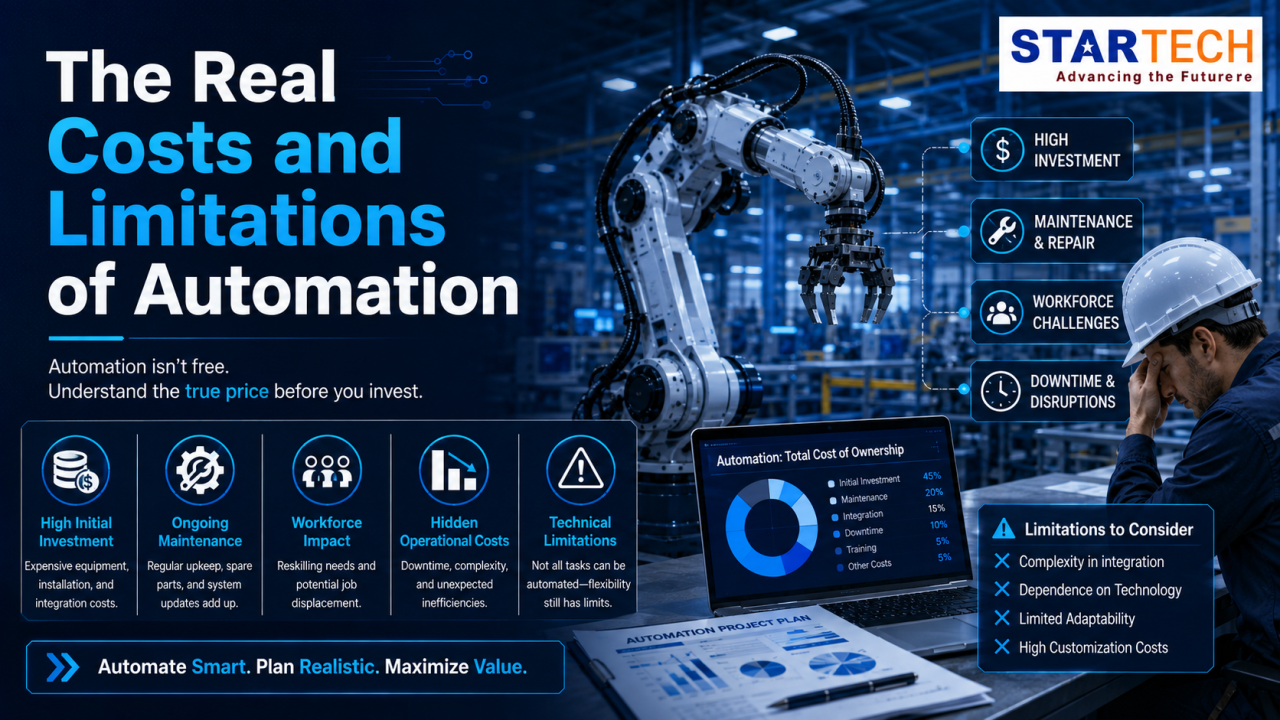
Any serious consideration of manufacturing automation process must evaluate the trade-offs involved, since ignoring them is a sure way to engineer a disaster.
Upfront costs. Automated processes require a large investment in robotic machinery and control systems. However, the equipment cost is only one part of the equation – often a small one at that – since installing them and retrofitting existing infrastructure to work with the new systems takes much longer and is far more expensive than anyone expects.
Integration time and complexity. New automated systems rarely exist in a vacuum. Installing robots means integrating them with legacy machines and control systems, which is much harder than most realize. The skills required for maintenance and programming are specialized, so unless a manufacturer is entirely self-sufficient with its maintenance and repair work, it will have to hire contractors for any automated machinery-related job.
Fixed automation is less flexible but usually faster, requiring less time and effort to produce a single unit. However, it is much harder to repurpose if the manufacturer wants to shift to another product that uses a different production process.
The threat of cyberattacks via control system networks. Connecting automated machines into a network, whether it is a factory LAN or the Internet for remote access and control, creates possibilities for exploitation that did not exist when the machines were standalone. Industrial control systems were never designed with security in mind, and that constitutes a risk to any manufacturer that connects them to a network, whether they realize it or not.
Downtime during installation or upgrades. Upgrading to a new automated process is seldom something a manufacturer can do without any production downtime, and that downtime always turns out to be more costly than budgeted. It can easily outweigh the benefits of automation during the first year or two after installation.
With all of these issues in mind, it should be apparent that automation is not a risk but rather an opportunity to be seized. The next section will discuss how the risk of those potential pitfalls can be reduced by preparing a realistic automation budget.
How an Automation Project Actually Unfolds
Manufacturing automation projects that succeed tend to follow a broadly similar sequence, even when the specific technology differs.
1. Process audit. Before selecting any equipment, map the process as it currently runs — cycle times, failure points, quality issues, and where operators spend the most time on low-value tasks. This step is frequently skipped in the interest of speed, and it is one of the most reliable ways to end up automating the wrong thing.
2. Define scope and success criteria. Decide specifically what the automation needs to achieve — a throughput target, a defect-rate reduction, a specific safety improvement — and how it will be measured. Vague goals make it impossible to judge whether the project actually worked.
3. Select the right level and type of automation. Match the automation approach (fixed, programmable, or flexible) and the specific technologies to the process characteristics identified in the audit, rather than defaulting to whatever a vendor is promoting.
4. Vendor and integrator selection. For most manufacturers, this means choosing a system integrator who can combine hardware from multiple suppliers into a working solution, not just a single equipment vendor. Track record with similar processes, protocol compatibility, and after-sales support all matter more than headline pricing.
5. Pilot before scaling. Running a contained pilot on one line or one process — rather than a full-facility rollout — surfaces integration problems while they are still cheap to fix. Skipping this step to save time is one of the most common ways a project ends up taking longer overall.
6. Commissioning and validation. Confirm the system performs to the defined success criteria under real production conditions, not just in isolated testing, before declaring the project complete.
7. Training and handover. Operators, maintenance technicians, and engineers need proper training on the new systems before the integrator’s support contract winds down. Under-investing here is one of the fastest ways to lose the reliability gains automation was supposed to deliver.
8. Scale and iterate. Once the pilot proves out, extend the approach to additional lines or processes, applying the lessons learned rather than repeating the same mistakes at larger scale.
Common Mistakes That Undermine Automation Projects
Automating a broken process. It will make the broken process much more efficient, but fixing the process and then automating will give exponentially better results.
Underestimating the work involved in connecting your new technology to the existing PLCs or SCADA systems or MESs. And if you think there is no difference between Modbus, PROFINET, EtherCAT or OPC UA – you are in for unpleasant surprises, which are much more expensive than most people realize.
Not considering the extensive and vital operator training as an essential part of the project. A system that isn’t utilized to its fullest potential due to operator misunderstanding will be significantly less effective.
Not considering cybersecurity from day one. Retrofitting existing control hardware/software with security features post-installation is far more involved and expensive than designing security functions into the system during development.
The desire to use state-of-the-art technologies to solve day-to-day challenges instead of using something old but proven. A self-learning AI system is not always the solution for a simple PLC task. The tendency to go for the fanciest tool for a particular job is a recurrent theme among many underperforming projects. The truth is that for most projects, a properly specified PLC is usually more cost-effective than using a full-blown adaptive control system.
Finally, skipping the pilot project. Because when you have a fully integrated process control system at your works – you don’t want to run any risks by not properly testing a new technology before rolling it out in production. But the costs of such complacency are often extremely high – as the problems will affect an entire production facility instead of just one machine.
Industry 4.0, Edge Computing, and Where the Technology Is Heading
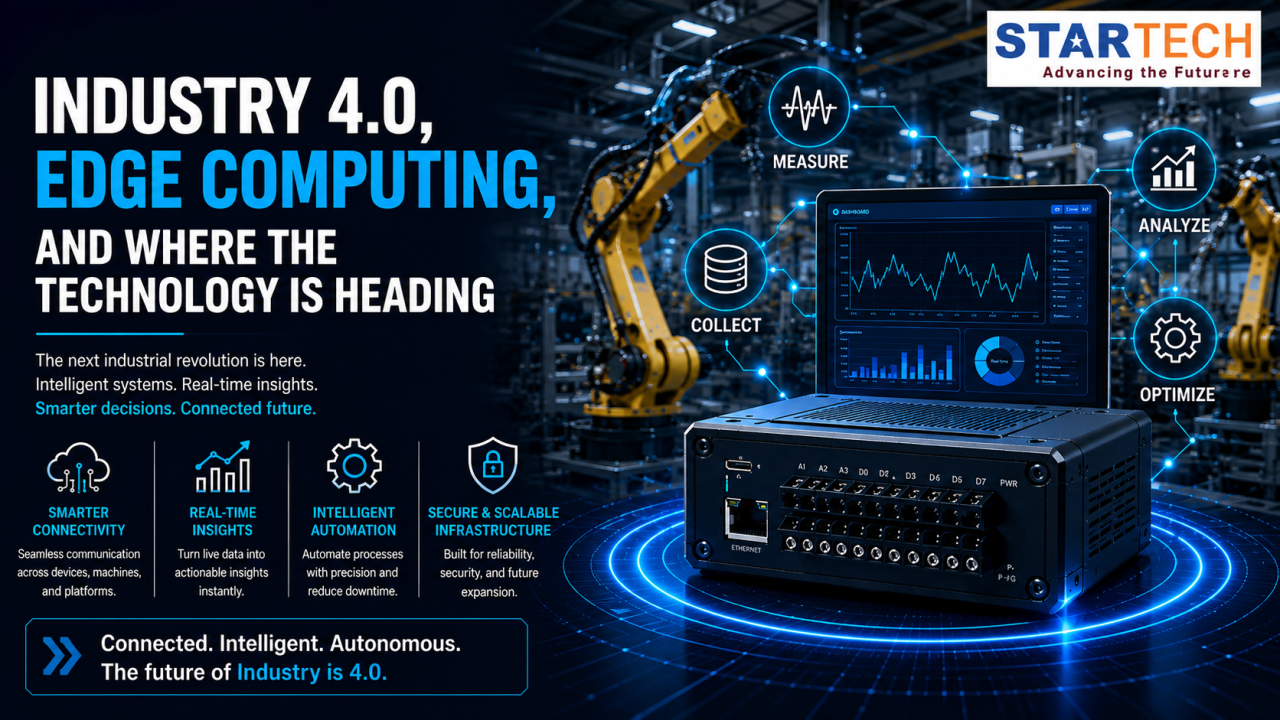
Industry 4.0 is often used as an umbrella term for a wide range of ideas that have little to do with each other. Industry 4.0 is best understood as a particular level of integration between automation, real-time data, and control systems that allows individual plants to operate with minimum human intervention. Automation is the foundation of this state, which is why true Industry 4.0 has never existed without it.
Edge computing is an interesting prospect for future automation in particular because of the ways it allows control systems to make decisions faster, closer to the process itself. Rather than sending data to a distant server for processing, an edge platform handles queries directly at the source. This has two key advantages in industrial automation: reduced bandwidth requirements for analytics-critical systems and increased reliability through decreased dependence on external infrastructure.
When choosing hardware for edge analytics, system integrators and panel builders considering this technology option would benefit from prioritizing mechanical endurance in high-heat environments, low-maintenance cooling, and compatibility with the industrial network protocols on-site.
AI-assisted automation is set to see practical applications in industrial settings in a limited number of use cases within the next few years. The two most promising areas are Predictive Maintenance, which identifies potential equipment failures before they occur, and quality control, where automation is used to identify previously undetectable flaws.
However, industrial control systems are not being replaced by anything more advanced anytime soon. Automation software that uses artificial intelligence to inspect or predict is not a panacea for control logic problems.
Digital twins are primarily used in model-driven automation to define processes before implementing changes on the shop floor. These virtual replicas are updated in real-time with data from physical counterparts, allowing engineers to study and optimize the reproduction of a process before making any adjustments in the real world. This reduces the risks and costs associated with trial-and-error automation projects.
Sustainability-focused automation is an upcoming trend driven by rising energy prices and regulatory pressures. Some systems emphasize energy recovery and consumption reduction over traditional productivity-centered approaches. This type of automation will have a significant impact on industrial plants where energy expenditure and production are directly linked.
None of these innovations eliminate the need for what was previously discussed in this series. On the contrary, all of these improvements serve to build on existing solutions that create long-term value, which is why looking into their development is a more rewarding investment of time than trying to keep up with the latest trends.
Automation in Manufacturing Across UAE-Relevant Industries
The role of automation can vary widely across industries, influencing the choice of solutions in each of them significantly.
Oil, gas, petrochemicals. The need for automation for such processes as pipeline transportation and refining has seen one of the longest developments in the history of the industry, as continuous high-volume processes benefit massively from having all aspects automated. SCADA systems that monitor and control the production process are among the most established forms of automation in this sector, with safety-critical systems on top of process control being an aspirational state for many other industries to reach.
Food and beverage. The automation of food production focuses on two main areas: achieving the necessary level of hygiene standard in all parts of the production process and maximizing output. This often results in wash-down rating, food-grade certification, and traceability being prioritized when automation is introduced to such a production facility, with filling and packaging lines receiving the largest amount of attention. Inspection systems that make sure that no incorrectly filled or labeled packages leave the facility comprise another large category.
Pharmaceuticals. Among the most highly regulated industries, pharmaceuticals have stringent requirements regarding traceability and process validation, making automation one of the preferred choices for most manufacturers, including those with relatively low production volumes. Serialization, which allows tracking each produced unit through the supply chain, is a critical consideration in this sector with automation being necessary to fulfill such requirements.
Automotive and industrial parts. The focus of automation in this industry is on achieving maximum precision, reliability, and flexibility, particularly at the high-end of the market. Original equipment manufacturers that provide components to car manufacturers worldwide have a strong advantage over competitors in terms of being able to document and control every step of the production process, which is needed for the sake of meeting the requirements of their customers.
Water treatment and utilities. While large-scale water treatment facilities and power plants are sites of intensive automation, many utilities have to manage their remote infrastructure with limited automation capabilities, meaning control and monitoring from a central location are often the only option. Edge computing solutions have seen an especially intense level of development for this sector, with remote operators being responsible for the continuous operation of pumping stations and water treatment facilities.
Metal fabrication and panel building. Companies that provide fabricated metal details and structures for other manufacturers that use automation are increasingly looking to adopt similar technologies to automate their own operations. This is particularly true for robotic welding, cutting, and assembly equipment, which fulfill the same purpose of reducing the workload on human workers.
The UAE Policy and Market Context
The UAE has made manufacturing automation a clear priority of its own, as the country seeks to reduce its dependence on hydrocarbons by pursuing an economic diversification policy. The UAE government’s interest in promoting industrialization as a way to grow the emirate’s GDP and international competitiveness is therefore evident.
This makes automation an indispensable, almost inevitable development in the United Arab Emirates, which has a limited domestic labor force that is not as highly trained as in other countries, unable to cope with menial or dangerous work.
Moreover, the tendency of the UAE to adopt very strict standards compared to other countries is another factor that makes automation much more common and important. The most obvious example is the food processing industry, which must adhere to extremely rigorous standards for both local and international markets, requiring automated systems to provide the necessary documentation and traceability.
It is therefore essential to consult the appropriate authorities and international partners on their requirements when developing systems in order to avoid having to re-engineer them later.
Choosing the Right Automation Partner
For procurement managers and plant leaders evaluating vendors, a few practical criteria consistently separate stronger partners from weaker ones.
Relevant process experience. A vendor or integrator who has worked on similar processes — not just similar industries — understands the specific failure points and integration challenges likely to come up, rather than learning them at your expense.
Protocol and systems compatibility. Confirm upfront that any proposed solution can communicate with existing PLCs, SCADA, or MES systems using protocols already in use on site. Protocol mismatches are one of the more common, and avoidable, sources of integration cost.
Local support and service response. Automated systems fail eventually, and how quickly a vendor can respond — with parts, technicians, or remote diagnostics — matters as much as the equipment specification itself, particularly for facilities running continuous processes.
Transparent total cost of ownership. A credible vendor will walk through installation, commissioning, training, spare parts, and ongoing support costs, not just the headline equipment price. Quotes that only cover hardware tend to understate the real project cost significantly.
Willingness to pilot. A vendor confident in their solution should be comfortable proposing a contained pilot rather than pushing directly for a full-facility rollout. Reluctance to pilot is often a signal worth taking seriously.
Cybersecurity Considerations for Connected Automation
As they grow more connected in order to realize the benefits of remote access, central data repositories, and links to MES and ERP systems, control systems require a higher degree of security by design. Systems that were previously engineered to meet standards of process reliability and safety in an isolated environment represent a huge vulnerability once exposed to a networked environment.
Some practical measures here include segmentation of OT networks from the main IT network, secure remote access, and maintaining an inventory of all devices on the network. For system integrators and panel builders, specifying and designing in security is a far more cost-effective measure than trying to retrofit existing systems with the required protection schemes later.
Conclusion
For manufacturers earlier in their automation journey, the most productive starting point is rarely the most ambitious one. Identify a single process with a clear, well-understood problem — a bottleneck, a recurring quality issue, a task with a genuine safety risk — and evaluate whether a contained automation investment addresses it.
That approach builds internal expertise, produces a measurable result, and creates a template that can be extended to other processes with far less risk than attempting a facility-wide transformation in one step.
Whatever stage an operation is at, the underlying pattern holds: automation in manufacturing pays off when it is applied to a well-understood process, planned with a realistic view of total cost, piloted before it is scaled, and supported by people trained to keep it running — not when it is treated as a single purchase that solves a problem on its own.
The technology itself is genuinely capable. What determines whether a project succeeds is almost always the planning and change management around it, not the hardware.
FAQ
1. What's the difference between automation and Industry 4.0?
Automation refers to using control systems and machinery to run production tasks with minimal manual intervention. Industry 4.0 is the broader integration of that automation with real-time data, connectivity, and analytics so a plant can adjust its own operations dynamically. Automation is the foundation; Industry 4.0 builds on top of it.
2. How much does manufacturing automation typically cost?
Manufacturing automation varies significantly by process, scale, and how much legacy integration is involved, which is why a credible quote requires a proper process audit first rather than a generic estimate. The bigger cost risk usually isn’t the headline equipment price — it’s underestimated engineering, commissioning, and downtime costs during installation.
3. Can small and mid-sized manufacturers afford automation?
Yes, particularly with the growth of collaborative robots and modular automation systems that don’t require the large upfront investment traditional industrial robotics historically did. A targeted pilot on one process is usually a more realistic starting point for smaller manufacturers than a full-line automation project.
4. Will automation replace factory jobs?
It tends to change the mix of jobs more than eliminate them outright — reducing demand for repetitive manual tasks while increasing demand for technicians who can program, maintain, and troubleshoot automated systems. Manufacturers that plan for this shift with training tend to see smoother adoption than those that don’t address it.
5. What industrial protocols should I plan for when specifying automation equipment?
Modbus, PROFINET, EtherCAT, and OPC UA are among the most common in current industrial automation deployments, though the right choice depends on what’s already running in the plant and what equipment vendors support. Getting protocol compatibility wrong is one of the more common — and avoidable — sources of integration cost.